




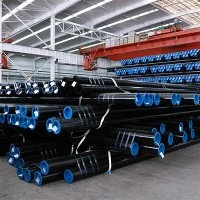


API 5L X52 Seamless and Welded Pipeline
API 5L X52 is a steel grade of API SPEC 5L (Line Pipe Specification), which is compiled and published by the American Petroleum Institute and includes seamless steel pipes and welded steel pipes for pipeline transportation systems in the oil and gas industry.GNEE supplies other grades: X42, X46, X52, X56, X60, X65, X70 Line Pipe for oil and gas transportation all over the world.
Advantages of API 5L X52 steel pipe:
API 5L X52 high-strength pipe has excellent strength and toughness. Its alloy composition has been carefully designed and optimized to enable it to maintain good stability and durability while withstanding high pressure and high temperature. This enables API 5LX52 carbon steel oil pipe to cope with various complex and harsh working environments in the fields of oil and gas, ensuring the safety and stable operation of the project. Secondly, API 5LX52 seamless corrosion-resistant pipe also has good corrosion resistance. Its surface has been specially treated to effectively resist the erosion of various corrosive media and extend its service life.
API 5L X52 pipeline grade:
Based on product specification grade: PSL1, PSL2
API 5L X52 PSL1, used for pipelines with common delivery conditions in the rolled state.
API 5L X52N/M/Q, used for PSL2 pipelines with delivery conditions of N, M and Q.
API 5L X52NS/MS/QS, used for PSL2 pipelines for sour service.
API 5L X52 Carbon Steel Pipeline Manufacturing Process
The API 5L X52 pipeline is manufactured from ingots, billets, billets, coils or plates using basic oxygen, electric furnaces or open hearth furnaces combined with ladle refining processes. For PSL2 grade, deoxidation and remelting treatments must be carried out in accordance with fine grain operation specifications. At the same time, repair welds are strictly prohibited for coils or plates used for PSL2 pipelines.
There are three types of welding methods for API 5L X52 pipelines: the first is ERW (electric resistance welding), which uses high-frequency current to heat and melt the edge of the steel strip to achieve welding; the second is LSAW (longitudinal submerged arc welding), which uses a submerged arc welding gun to weld the inner and outer sides of the longitudinal tube after the steel plate is rolled into a tube; the third is SSAW (spiral submerged arc welding), which uses a submerged arc welding process to weld the steel plate along the spiral line after the steel plate is rolled into a tube.
API 5L X52 PSL1 Pipe Chemical Composition
| CHEMICAL COMPOSITION | ||||||
| Mass fraction, based upon heat and product analysis a | ||||||
| SEAMLESS PIPE | ||||||
|
C |
Mn |
P |
S |
V |
Nb |
Ti |
|
maxb |
max.b |
max. |
max. |
max. |
max. |
max. |
|
0.28 |
1.40 |
0.030 |
0.030 |
d |
d |
d |
|
WELDED PIPE |
||||||
|
0.26 |
1.40 |
0.030 |
0.030 |
d |
d |
d |
| a 0.50% maximum for copper, 0.50% maximum for nickel, 0.50% maximum for chromium, and 0.15% maximum for molybdenum. | ||||||
| b For each reduction of 0.01% below the specified maximum concetration for carbon, an increase of 0.05% above the specified maximum concentration for manganese is permissible, up to a maximum of 1.65% | ||||||
| c unless otherwise agreed, the sum of the niobium and vanadium contents shall be ≤0.06%. | ||||||
| d The sum of the niobium ,vanadium and titanium concentratons shall be ≤0.06%. | ||||||
| e Unless otheriwse agreed. | ||||||
| f unless otherwise agreed, the sum of niobium, vanadium and titanium concentrations shall be ≤ 0.15% | ||||||
API 5L X52 PSL1 Pipe Mechanical Properties
|
AVG ABSORBED ENERGY |
IND. ABSORBED ENERGY |
|
27 MIN (JOULES) |
20 MIN (JOULES) |
|
IMPACT TEST |
|
|
Yield Strength (R10.5) |
Tensile Strength (R) |
|||||||
|
PSL |
Mpa |
PSL |
Mpa |
|||||
|
52,200 |
360 Min |
66,700 |
460 Min |
|||||
|
MECHANICAL PROPERTIES |
||||||||
API 5L Pipe grades, Steel grades and acceptable delivery conditions
| Information | About |
|
Surface |
surfaces are 100% visually inspected. The surface are according to API 5L standards. External surface : covered with varnish. |
|
NDT |
Pipes are ultrasonic tested with respect to API 5L standards: longitudinal: 100% surface of pipe Note: pipe ends not scanned by automatic ultrasonic system Pipe Ends are manual Inspected UT / Magnetic Particle Examination. |
|
Certification and traceability |
Every dimensions Pipes are supplied with a 3.2 certificate acc. EN 10204, Marking : SI units (X52) with respect to API requirements & mill standard. |
|
Dimensional control |
Every dimensions will be supplied with respect to API 5L Body Of Pipe will be +/- 0,75% End Of Pipe will be +/- 0,5% Wall thickness of Pipe will be +15%, -12,5% Length of Pipe will be -0 / +100mm |
|
Pipe Ends |
Pipe Ends are beveled. End angles : 30°- 0°/+5°, root face : 1.6mm +/- 0.8mm |
|
Protection |
Pipes Outer Sides are Vanished. |
API X52 Steel Pipe Processing Services

Gnee Factory environment

Gnee Packaging and shipping

Hot Tags: API 5L X52 Seamless and Welded Pipeline, China API 5L X52 Seamless and Welded Pipeline manufacturers, suppliers, factory, api 5l line pipe for long distance transmission, api 5l line pipe for harsh environments, api 5l grade x52 pipe, api 5l grade x56 pipe, line pipe supplier, api 5l pipe for lubricant transportation
You Might Also Like


Send Inquiry